
Line Clearance Was Completed—Why Did the Previous Batch Label Reach the Next Run?
Line clearance was completed—why did the previous batch label reach the next run?
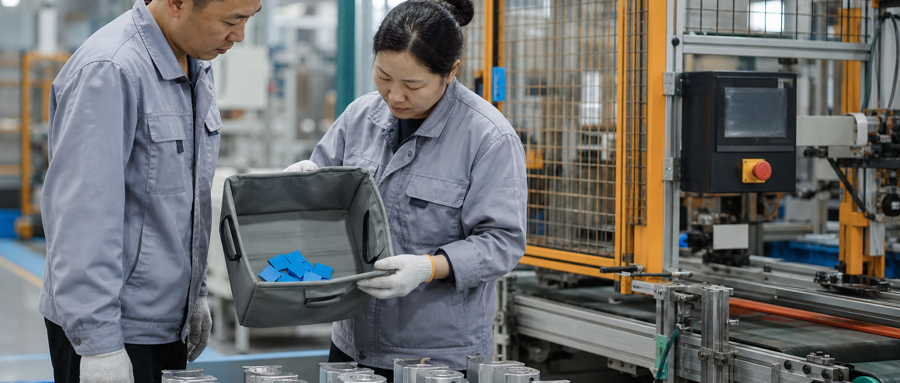
In the afternoon, the team moved to the next batch, pushing the previous batch of finished products away and cleaning the workbench. However, after the new batch started up for half an hour, the inspector found several old labels at the bottom of the tote box. The products were correct, but their identity might have been mislabeled, forcing the entire batch to be halted for verification.
This is a common high-risk scenario in packaging, assembly, and multi-product mixed-line factories. What the factory owner sees is just a piece of paper, but the frontline faces batch isolation, customer traceability, and rework costs.
The issue often lies not in whether the employees cleaned up, but in the fact that the clearance only checked visible surfaces, without confirming that the previous batch's products, labels, documents, and system tasks had all been removed from the shop floor.
Cleaning Is Complete, But the Previous Batch Hasn't Actually Left
Ordinary cleaning focuses on dust, waste, and tool placement; however, line clearance must also answer four questions: whether the previous products have been cleared, old labels have been retrieved, old documents have been removed, and old tasks have been closed.
If any of these items remain at the workstation, the new batch may inherit the identity of the previous one. Especially small items like loose labels, reprinted labels, and temporary rework orders are easy to hide in printer trays, tote box compartments, and drawers due to their small size and fast movement.
The U.S. pharmaceutical production regulations require checking the work area before packaging and labeling to confirm that products, documents, and materials from the previous operation have been removed, and the inspection results should be recorded in the batch record. Although industries differ, this control logic is worth adopting in general manufacturing environments.
Real Loopholes Often Occur in the "Last Few"
A total of 100 labels were issued from the label warehouse, with 98 used shop-floor. The remaining two labels, if only marked as 'cleared,' still pose risks. The numbers for issuance, usage, disposal, and return must align.
Another vulnerability lies in print permissions. Although old paper labels were removed, old batch numbers remain printable in the system. When employees reprint a label, selecting the wrong task can result in the previous batch label reappearing shop-floor.
The FDA inspection guide emphasizes that specific batches in manufacturing, packaging, labeling, and control must be documented. The value of records is not for accountability but to enable shop-floor responses to questions such as where old labels went, who reviewed them, and when the batch was closed.
Turn Clearing into an Identity Switch
The first step is to perform a physical zeroing out. Check the interiors of the equipment, conveyor lines, printers, workbenches, returnable containers, and garbage containers along a fixed route, and confirm old products, old labels, and old documents separately.
Second, achieve numerical closure. Record the issuance, usage, disposal, and return of labels by batch. If numbers do not match, identify discrepancies first and prevent the new batch from starting. For factories unable to track each label, they must still be responsible for full rolls of labels and reprint records.
Third, perform a system switch. Close old work orders and old print tasks before opening new batches. Ensure terminals only accept the current batch, intercepting old batches immediately. A simple, dismissible prompt is insufficient.
Step four involves dual verification. The operator is responsible for line clearance, and the next position or shift leader conducts a recheck along the same route. The verifier is not just a signature machine; they must be able to see label differences and system status.
Operators fear line stoppage and responsibility, shift leaders are concerned with output, and quality has responsibility but lacks authority. If no one takes ownership, transfers, handles, escalates, or closes issues, the shop floor will produce less and make fewer errors. The plant manager must authorize quality to freeze batches with unbalanced data and separate compliance clearance from efficiency penalties.
Start with the Most Confusing Line First
Small factories can use a single clearance checklist and label transfer bag; medium-sized factories connect work orders, print tasks, and identity verification; mature factories add label permissions, abnormal freezing, and batch traceability.
Not all factories need to implement this all at once. Factory owners can forward inspections to plant managers, quality supervisors, and shift leaders, and only review three signals weekly: whether label differences are closed, whether reprints have reasons, and whether old batch materials are still found after clearance.
The standard for line clearance during changeover is not just clean floors and tidy workbenches, but that the previous batch can no longer enter the next one. Elevating cleaning to a status switch ensures old labels do not suddenly appear after the new batch starts up.
I am Huang Chaoxing, inventor of the TreeMES stack-light MES system. Follow me for insights into the management logic behind frontline stories in manufacturing.
