
Inspection Rejected the Batch—Why Did It Still Move to the Next Operation?
At 9 a.m., a quality inspector marked a batch of bushings as nonconforming in the system due to excessive inner hole dimensions. By 10:30 a.m., the assembly line found that the batch had already been issued, with over 20 pieces loaded into semi-finished goods. The warehouse stated they only saw available inventory, the team leader mentioned there was no clear marking on the material box, and the quality inspector confirmed the inspection report had already been submitted.
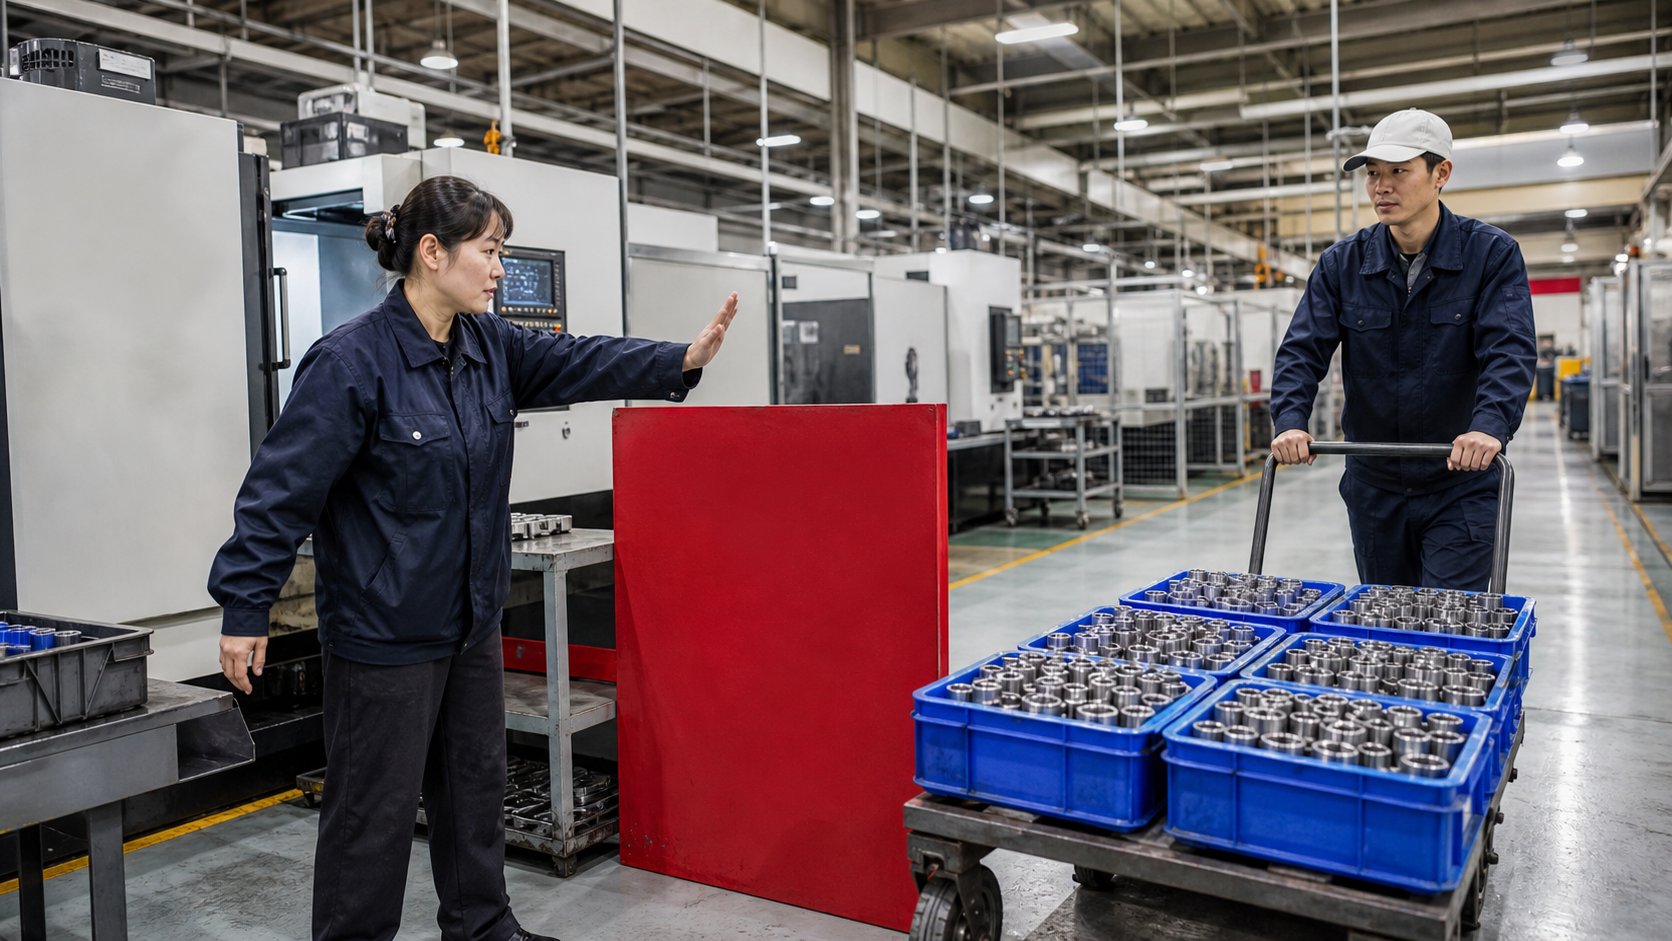
The inspection order has been rejected, why does this batch of materials still flow to the next process?
At 9 a.m., a quality inspector marked a batch of bushings as nonconforming in the system due to excessive inner hole dimensions. By 10:30 a.m., the assembly line found that the batch had already been issued, with over 20 pieces loaded into semi-finished goods. The warehouse stated they only saw available inventory, the team leader mentioned there was no clear labeling on the material box, and the quality inspector confirmed the inspection report had already been submitted.
A rejection notice failed to stop the physical flow of materials. The issue is often not due to an individual's carelessness, but rather because the factory treats the 'inspection result' as the end of the quality loop. A true loop requires the batch status, storage location, material issuance authority, and disposal responsibility to change simultaneously. Otherwise, even if the system marks it as nonconforming, the physical site may still treat it as regular material.
For factory owners, the most important thing to look at is not who takes responsibility first, but which permissions and responsibilities are misaligned. In reality, doing more leads to more mistakes, and doing less leads to fewer mistakes, which may encourage people to prioritize self-protection: the warehouse refuses to accept orders, quality does not transfer, and the shop floor does not escalate issues, eventually leading to no one wanting to handle or close the abnormal situation.
1. Rejection is only a conclusion, not an isolation action
A quality inspector has the authority to issue inspection results but may not have the authority to lock the storage location, cancel the material issuance order, or halt the process. The warehouse bears the pressure of complete kits and material issuance. If the inventory status is not synchronized and frozen, issuing materials according to the order is the safest option. When team leaders are focused on production, they may prefer to trust the physical materials already delivered to the line.
This misalignment is most common in mid-sized growing factories: the system division of labor has been established, but cross-departmental actions still rely on verbal reminders. Small factories may rely on labels and WeChat groups, while large factories may have quality, warehouse, and production systems separated, leading to the conclusion being passed, but the execution status not being passed along.
2. The same batch of materials must have only one executable state
A batch of materials cannot simultaneously be marked as 'rejected' in the quality ledger, 'available' in inventory, and 'pending issuance' in the material issuance order. What the shop floor truly needs is not more statuses, but a main status that can directly determine the next action.
Recommend compressing the status into pending inspection, conforming, isolated, concession pending, return, or scrap. Once a rejection decision takes effect, the system first freezes the available quantity, and then the physical items are moved to the isolation area on site; before completing these two steps, the status remains 'isolation incomplete' and cannot be prematurely closed.
Batch number, container, and location must also be verified together. Only changing the system color without moving the physical items may allow forklifts to still transport old containers; only affixing a red tag without freezing inventory may result in the next material withdrawal order hitting the same batch again.
3. Link four time points into a chain of facts
The first is the time the inspection conclusion takes effect, the second is the inventory freeze time, the third is the physical isolation time, and the fourth is the final disposal time. Each step must have a responsible role and acknowledgment, with automatic reminders to the next level of responsibility if the time is exceeded.
If nonconforming items have already entered the next operation, the impact range must be immediately locked down: how many were used, which semi-finished products they entered, which workstations need to be stopped, and who decides on rework or scrap. It is not sufficient to only isolate the remaining inventory; the portion that has already flowed out must not be left for the shop floor to find slowly.
4. The factory owner only randomly checks three batches of materials every week
Select the three most recent rejection records and ask the system when the freeze occurred, when the physical items were moved, and whether the downstream received the impact list. If any of these times cannot be answered, it indicates that the rejection is still confined within the quality department.
A checklist can be used for a review: first, verify whether the rejected batch was frozen, second, check whether the physical items have left the conforming area, and third, confirm whether the downstream received the impact scope and disposal responsibility.
This approach is more suitable for discrete manufacturing plants with clear batch management and frequent coordination between warehouse and production. Regulated industries must also comply with their own regulations and procedures, but the fundamental principles remain the same: identification, recording, isolation, evaluation, and disposition should not be disconnected from each other.
The value of a quality conclusion lies not in adding another nonconforming item to the report, but in ensuring that nonconforming products truly stop moving forward from that moment. Locking in status, physical items, permissions, and responsibilities simultaneously can transform a rejection decision from a mere conclusion into an shop-floor action.
I am Huang Chaoxing, inventor of the TreeMES stack-light MES system. Follow me for in-depth insights into the management logic behind frontline stories in manufacturing.
