
From Trial Production to Mass Production: Align Product, Process and Release Records
The sample pieces passed inspection, and the customer confirmed mass production was feasible. However, once the first batch of production orders was issued, the shop floor discovered that the material batch had changed, the tooling was not locked, and the inspection was still based on temporary requirements from the trial production phase.
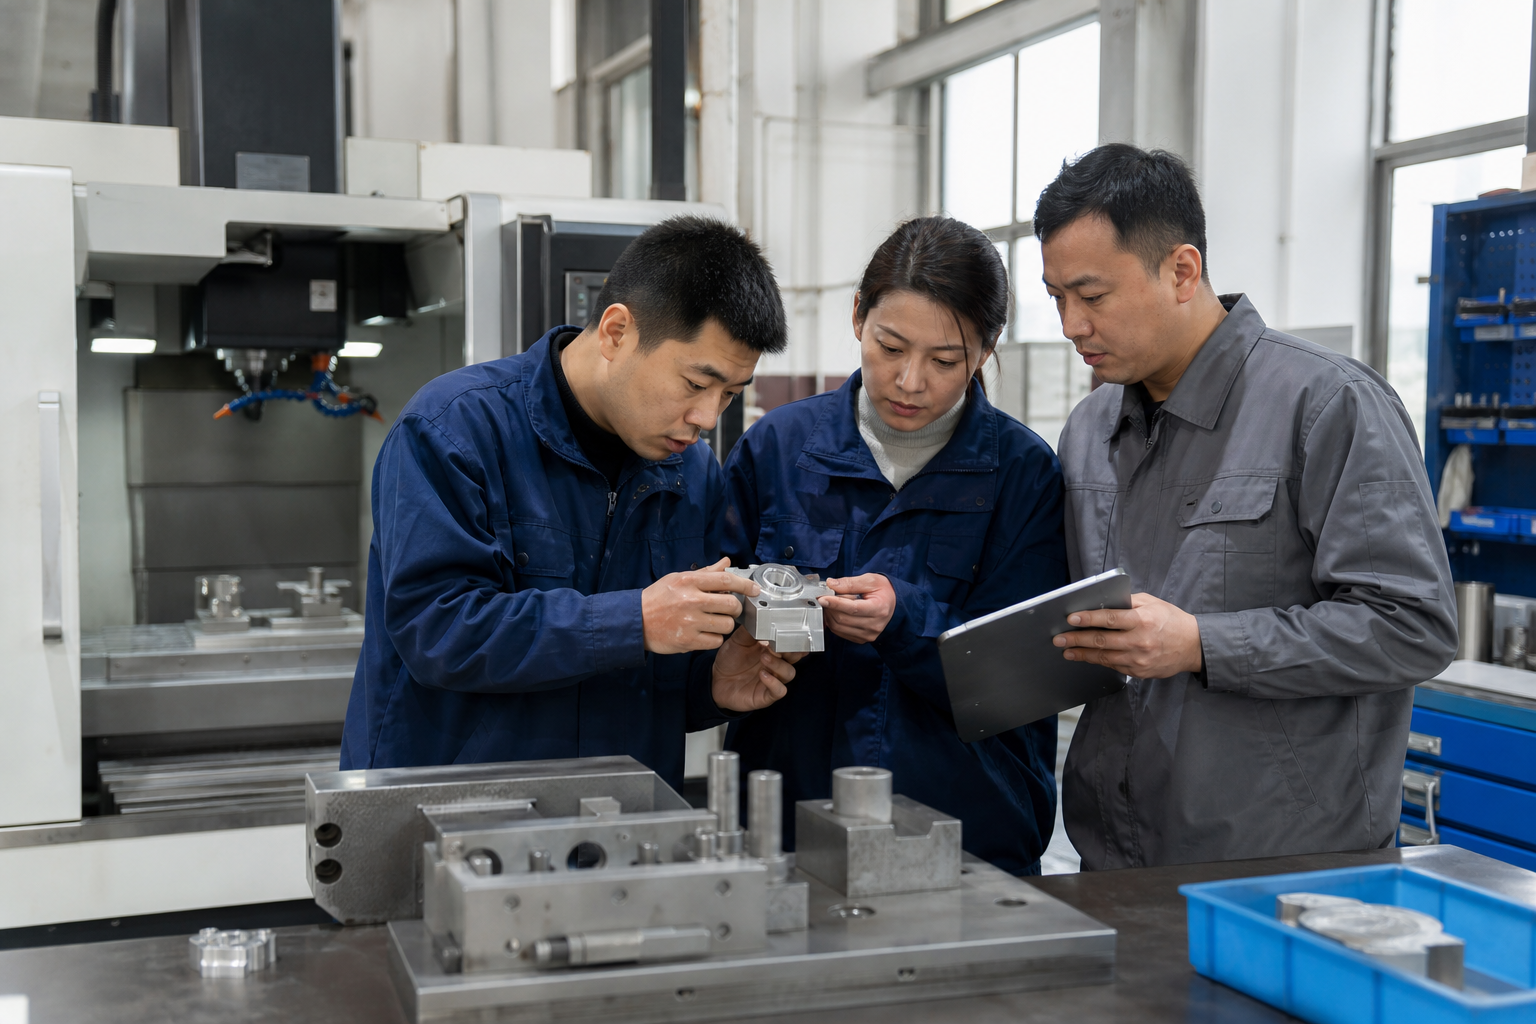
After the sample pieces pass inspection and the customer confirms they can proceed to mass production, the shop floor discovers issues when the first batch of orders is issued: material batches have changed, tooling is not locked, and inspection is still based on temporary requirements from the trial phase.
Passing trial production only proves that conforming parts can be produced under a specific set of conditions. Mass production requires demonstrating that the factory can consistently replicate the same results across different shifts, batches, and times.
Before transitioning to mass production, it is better to align the product record, process record, and release record item by item rather than holding a general review meeting. If any of the three records is not aligned, the first batch of mass production should be put on hold until confirmation.
Book One: Product Account Answers 'What to Do?'
First, lock in the formal versions of drawings, 3D models, technical requirements, bill of materials, and any customer-specific requirements. Do not just write 'based on the latest version'; record the specific version number, effective date, and replacement relationships.
Next, review temporary deviations from the trial phase. Actions such as manual adjustments, temporary material changes, or relaxed inspection criteria taken to expedite sample production must be clearly canceled, formalized, or continued under control. They should not be quietly carried over into mass production.
NIST's digital thread research highlights that product definitions should link design to manufacturing and quality, with inspection and measurement results fed back to design. The value of a product ledger lies in enabling all positions to work around the same authoritative definition.
Book Two: Process Account Answers 'What Enables Stable Replication?'
List equipment, tooling, procedures, process parameters, work methods, and personnel qualifications. Trial production is completed by experienced technicians, which does not imply that regular production crews have the same capability.
Write critical parameters as verifiable baselines, specifying allowable adjustment ranges, adjustment permissions, and rollback procedures. Only saving the final program without change records makes it difficult to explain differences between batches later.
NIST's research on manufacturing capability indicates that equipment and process capabilities change with system and decision-making scenarios. Therefore, mass production reviews cannot only focus on equipment names but must also check whether current capabilities match product requirements.
Book Three: Release Account Answers 'What Must Be Seen Before Proceeding?'
The first batch of mass production should clearly define inspection items, frequency, samples, and judgment rules for first-off, patrol checks, final pieces, or key processes. Measurement tools, procedures, and inspection versions should also align with the product ledger.
Define the isolation scope after an anomaly occurs: from which time point, which equipment, and which batch to hold for judgment; who confirms the cause, who approves resumption, and what additional verification is needed after resuming production.
NIST's experimental findings on integrating design, manufacturing, and inspection information reveal that lifecycle data is not easily automatically connected. For factories, this means that 'having it in the system' does not necessarily imply that upstream and downstream processes are using the same object and version.
Mass Production Meeting Makes One-Time Item-by-Item Decision
Create a checklist for the three accounts, listing 'confirmed', 'pending confirmation', and 'not applicable'. Pending items must have a responsible person, deadline, and evidence of closure; they cannot be dismissed with a vague statement like 'to be improved later'.
Small factories can start with a single table for management, while growing mid-sized factories should integrate version, batch, and approval status into the system. Mature factories should focus on preventing version misalignment between system interfaces.
Factory owners should focus not on passing the trial production once, but on whether the mass production conditions have truly been handed over to regular production teams. If success is credited only to R&D and all anomalies are blamed on production, the shop floor will develop a culture of doing more leading to more errors.
Not all factories need to establish a dedicated committee. Small factories can have one person authorized by the plant manager to consolidate information, clearly define job responsibilities, risk escalation, cross-departmental handover, and closure rules, to prevent collaboration from becoming an additional burden.
After the first batch, review the three accounts again: which conditions fail after shift change, which inspections failed to block defects, and which temporary actions were mistakenly considered standard. Rebase these differences to the baseline before the second batch can truly enter mass production.
I am Huang Chaoxing, inventor of the TreeMES stack-light MES system. Follow me for more practical factory-management methods.
